

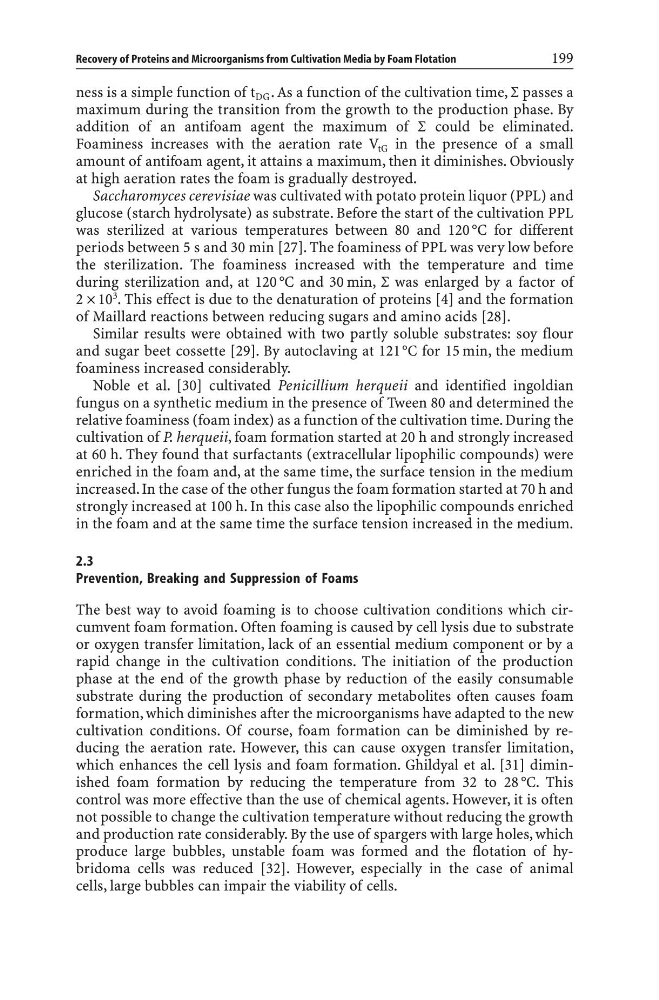
ness is a simple function of t DG . As a function of the cultivation time, S passes a
maximum during the transition from the growth to the production phase. By
addition of an antifoam agent the maximum of S could be eliminated.
Foaminess increases with the aeration rate V tG in the presence of a small
amount of antifoam agent, it attains a maximum, then it diminishes. Obviously
at high aeration rates the foam is gradually destroyed.
Saccharomyces cerevisiae was cultivated with potato protein liquor (PPL) and
glucose (starch hydrolysate) as substrate. Before the start of the cultivation PPL
was sterilized at various temperatures between 80 and 120 °C for different
periods between 5 s and 30 min [27]. The foaminess of PPL was very low before
the sterilization. The foaminess increased with the temperature and time
during sterilization and, at 120 °C and 30 min, S was enlarged by a factor of
2 ¥ 10 3 . This effect is due to the denaturation of proteins [4] and the formation
of Maillard reactions between reducing sugars and amino acids [28].
Similar results were obtained with two partly soluble substrates: soy flour
and sugar beet cossette [29]. By autoclaving at 121°C for 15 min, the medium
foaminess increased considerably.
Noble et al. [30] cultivated Penicillium herqueii and identified ingoldian
fungus on a synthetic medium in the presence of Tween 80 and determined the
relative foaminess (foam index) as a function of the cultivation time. During the
cultivation of P. herqueii, foam formation started at 20 h and strongly increased
at 60 h. They found that surfactants (extracellular lipophilic compounds) were
enriched in the foam and, at the same time, the surface tension in the medium
increased. In the case of the other fungus the foam formation started at 70 h and
strongly increased at 100 h. In this case also the lipophilic compounds enriched
in the foam and at the same time the surface tension increased in the medium.
2.3
Prevention, Breaking and Suppression of Foams
The best way to avoid foaming is to choose cultivation conditions which circumvent foam formation. Often foaming is caused by cell lysis due to substrate
or oxygen transfer limitation, lack of an essential medium component or by a
rapid change in the cultivation conditions. The initiation of the production
phase at the end of the growth phase by reduction of the easily consumable
substrate during the production of secondary metabolites often causes foam
formation, which diminishes after the microorganisms have adapted to the new
cultivation conditions. Of course, foam formation can be diminished by reducing the aeration rate. However, this can cause oxygen transfer limitation,
which enhances the cell lysis and foam formation. Ghildyal et al. [31] diminished foam formation by reducing the temperature from 32 to 28 °C. This
control was more effective than the use of chemical agents. However, it is often
not possible to change the cultivation temperature without reducing the growth
and production rate considerably. By the use of spargers with large holes, which
produce large bubbles, unstable foam was formed and the flotation of hybridoma cells was reduced [32]. However, especially in the case of animal
cells, large bubbles can impair the viability of cells.
Recovery of Proteins and Microorganisms from Cultivation Media by Foam Flotation
199