

1.3 Research on Weld Pool Behavior in Laser Welding
17
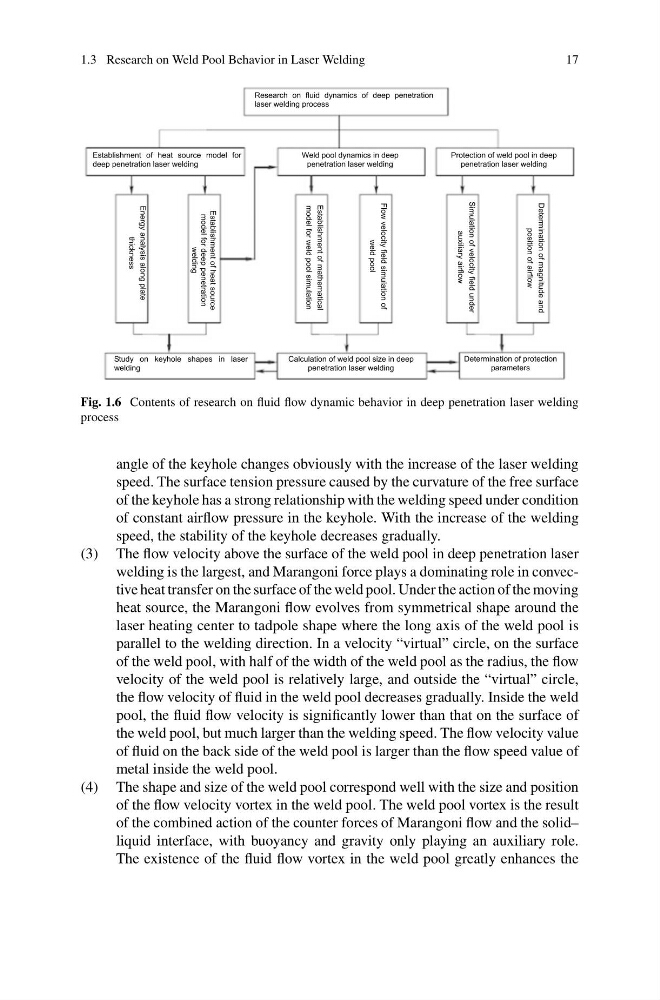
Fig. 1.6 Contents of research on fluid flow dynamic behavior in deep penetration laser welding
process
angle of the keyhole changes obviously with the increase of the laser welding
speed. The surface tension pressure caused by the curvature of the free surface
of the keyhole has a strong relationship with the welding speed under condition
of constant airflow pressure in the keyhole. With the increase of the welding
speed, the stability of the keyhole decreases gradually.
(3) The flow velocity above the surface of the weld pool in deep penetration laser
welding is the largest, and Marangoni force plays a dominating role in convective heat transfer on the surface of the weld pool. Under the action of the moving
heat source, the Marangoni flow evolves from symmetrical shape around the
laser heating center to tadpole shape where the long axis of the weld pool is
parallel to the welding direction. In a velocity “virtual” circle, on the surface
of the weld pool, with half of the width of the weld pool as the radius, the flow
velocity of the weld pool is relatively large, and outside the “virtual” circle,
the flow velocity of fluid in the weld pool decreases gradually. Inside the weld
pool, the fluid flow velocity is significantly lower than that on the surface of
the weld pool, but much larger than the welding speed. The flow velocity value
of fluid on the back side of the weld pool is larger than the flow speed value of
metal inside the weld pool.
(4) The shape and size of the weld pool correspond well with the size and position
of the flow velocity vortex in the weld pool. The weld pool vortex is the result
of the combined action of the counter forces of Marangoni flow and the solid–
liquid interface, with buoyancy and gravity only playing an auxiliary role.
The existence of the fluid flow vortex in the weld pool greatly enhances the