

248
8 Keyhole and Weld Pool Dynamics in Laser Welding with Filler Wires
Based on the discussion above, the following conclusions can be drawn: ➀ The
dynamic properties of the downward high-speed fluid caused by the recoil pressure on the wall surface of the keyhole are the primary factors that facilitate the
deep permeation of wire compositions into the work piece; ➁ Similar to the dilution behavior of the quasi-steady moving weld pool, the wire compositions, driven
by fluid dynamics that bypasses the keyhole, will concentrate on both sides of the
upper part of the weld joint, leading to the formation of local high concentration
areas; ➂ Under certain conditions, there will be an area with a high concentration of
wire compositions on both sides of the middle and lower parts of the weld joint; ➃
Convection is still the primary factor in the dynamic dilution of wire compositions
in the moving weld pool.
8.5.3.2 Influence of Technical Parameters on Distribution of Wire
Compositions in the Weld Joint at the Moment of Solidification
Based on the transient numerical model established in the previous section, the
influence of different technical parameters (laser power and welding speed) on the
distribution of wire compositions in the weld joint in the solidification instant is
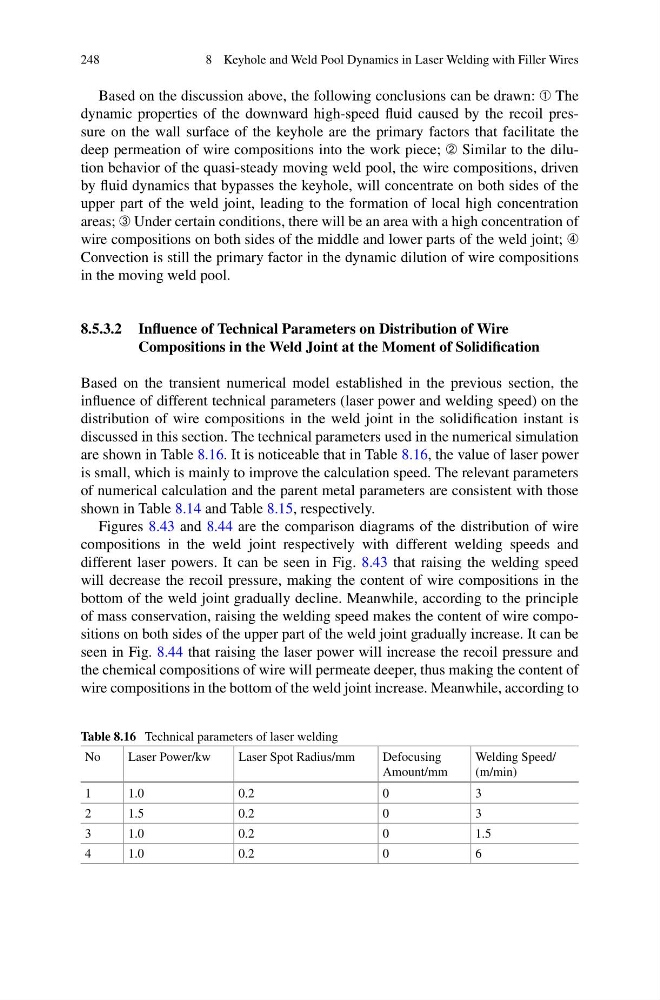
discussed in this section. The technical parameters used in the numerical simulation
are shown in Table 8.16. It is noticeable that in Table 8.16, the value of laser power
is small, which is mainly to improve the calculation speed. The relevant parameters
of numerical calculation and the parent metal parameters are consistent with those
shown in Table 8.14 and Table 8.15, respectively.
Figures 8.43 and 8.44 are the comparison diagrams of the distribution of wire
compositions in the weld joint respectively with different welding speeds and
different laser powers. It can be seen in Fig. 8.43 that raising the welding speed
will decrease the recoil pressure, making the content of wire compositions in the
bottom of the weld joint gradually decline. Meanwhile, according to the principle
of mass conservation, raising the welding speed makes the content of wire compositions on both sides of the upper part of the weld joint gradually increase. It can be
seen in Fig. 8.44 that raising the laser power will increase the recoil pressure and
the chemical compositions of wire will permeate deeper, thus making the content of
wire compositions in the bottom of the weld joint increase. Meanwhile, according to
Table 8.16 Technical parameters of laser welding
No
Laser Power/kw
Laser Spot Radius/mm
Defocusing
Amount/mm
Welding Speed/
(m/min)
1
1.0
0.2
0
3
2
1.5
0.2
0
3
3
1.0
0.2
0
1.5
4
1.0
0.2
0
6