

Solution Combustion Synthesis of Calcium …
193
0
1 0
2 0
3 0
4 0
0.0
0.1
0.2
0.3
0.4
0.5
0.6
Co-efficient of friction
(a)
(b)
(c)
7N
(a) - Ti6Al4V substrate
(b) - sample a1
(c) - sample a2
0
1 0
2 0
3 0
4 0
0.0
0.1
0.2
0.3
0.4
0.5
0.6
Co-efficient of friction
(a)
(c) (b)
5N
(a) - Ti6Al4V substrate
(b) - sample a1
(c) - sample a2
0
1 0
2 0
3 0
4 0
0.0
0.1
0.2
0.3
0.4
0.5
0.6
Sliding distance (meter)
Co-efficient of friction
(a) - Ti6Al4V substrate
(b) - sample a1
(c) - sample a2
(a)
(c)
(b)
1N
0
1 0
2 0
3 0
4 0
0.0
0.1
0.2
0.3
0.4
0.5
0.6
Sliding distance (meter)
Co-efficient of friction
(a)
(c)
(b)
2N
(a) - Ti6Al4V substrate
(b) - sample a1
(c) - sample a2
(a) -Ti-6Al-4V substrate
(b) - coating (a1)
(c) - coating (a2)
(c) - coating (a2)
(a) -Ti-6Al-4V substrate
(b) - coating (a1)
(c) - coating (a2)
(a) -Ti-6Al-4V substrate
(b) - coating (a1)
(c) - coating (a2)
(a) -Ti-6Al-4V substrate
(b) - coating (a1)
Sliding distance (meter)
Sliding distance (meter)
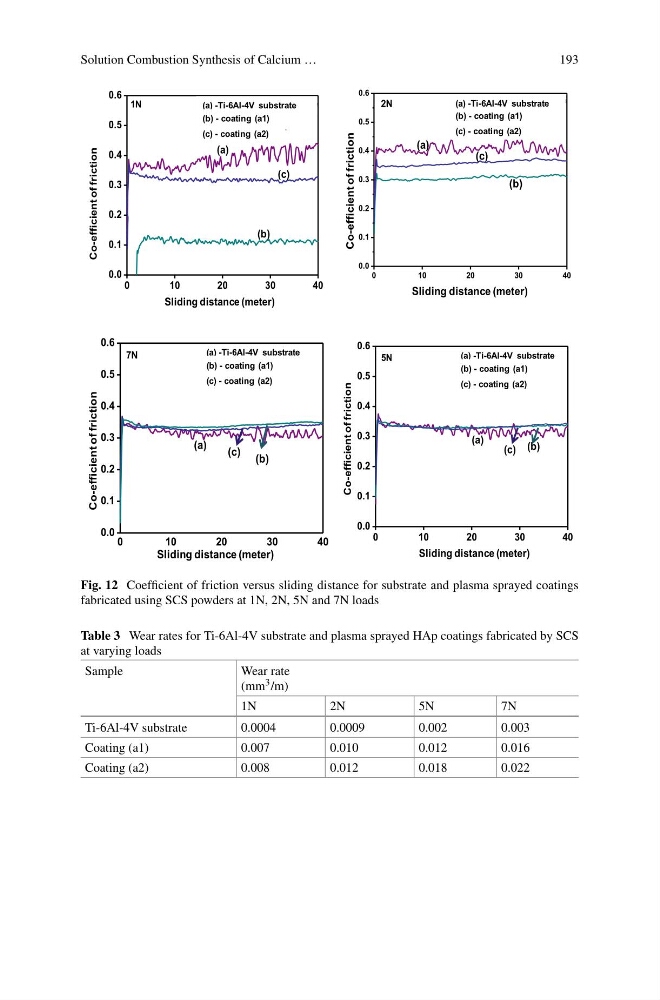
Fig. 12 Coefficient of friction versus sliding distance for substrate and plasma sprayed coatings
fabricated using SCS powders at 1N, 2N, 5N and 7N loads
Table 3 Wear rates for Ti-6Al-4V substrate and plasma sprayed HAp coatings fabricated by SCS
at varying loads
Sample
Wear rate
(mm 3 /m)
1N
2N
5N
7N
Ti-6Al-4V substrate
0.0004
0.0009
0.002
0.003
Coating (a1)
0.007
0.010
0.012
0.016
Coating (a2)
0.008
0.012
0.018
0.022