

282
M. F. Makhtar et al.
Table 25.1 Welding
parameters
Process Parameters
Values
Tool rotational speed (rpm)
490, 910 and 1700
Welding speed (mm/s)
16, 29 and 44
Tool tilt angle (°)
2
Tool Shoulder Diameter (mm)
20
Tool Shoulder surface
Flat
Pin Length (mm)
7
Pin Profile
Standard cone
Tool Material
High Carbon steel (H13)
available on this machine enabled the joining to occur. Table 25.1 indicates the
welding parameters used in the experiment. The plate was cut into two sections
consisting of horizontal and vertical plates. The dimension of the horizontal plate
was 158 mm x 137 mm x 5 mm, while the dimension of the vertical plate was 158 mm
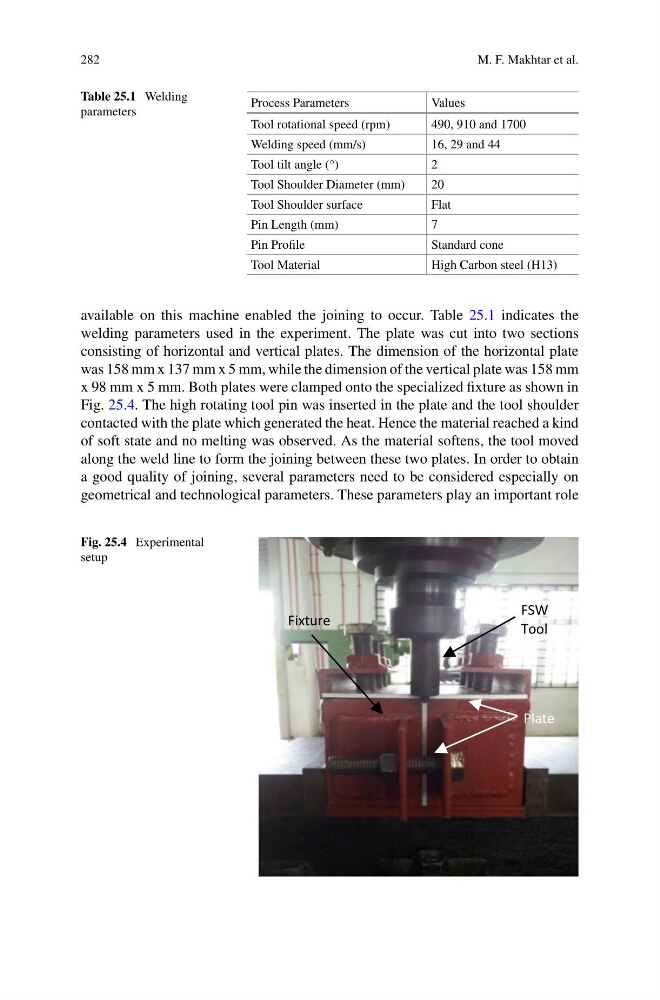
x 98 mm x 5 mm. Both plates were clamped onto the specialized fixture as shown in
Fig. 25.4. The high rotating tool pin was inserted in the plate and the tool shoulder
contacted with the plate which generated the heat. Hence the material reached a kind
of soft state and no melting was observed. As the material softens, the tool moved
along the weld line to form the joining between these two plates. In order to obtain
a good quality of joining, several parameters need to be considered especially on
geometrical and technological parameters. These parameters play an important role
Fig. 25.4 Experimental
setup
FSW
Fixture
Tool
Plate