

645
The measured methane concentration curves before and after the pressure compensation
(at 20% methane) over a pressure range from 30 kpa to 200 kpa are shown in Figure 3.
It can be seen that the measurement accuracy is improved with the use of the pressure
compensation within the pressure range of 30–200 kpa.
4 FIELD TRIALS AND RESULTS
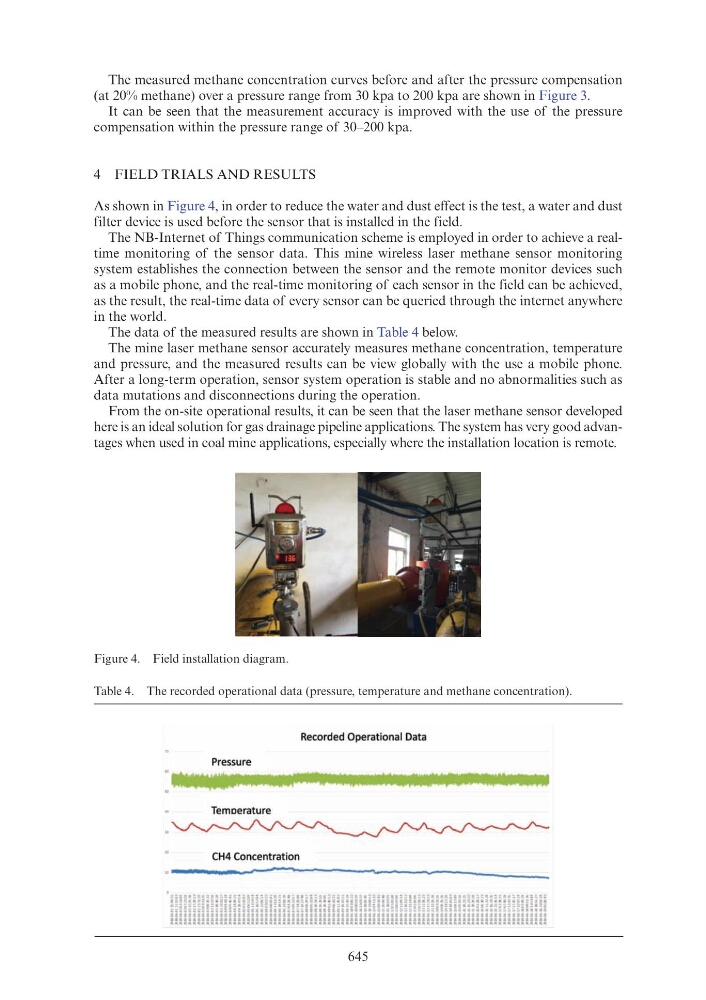
As shown in Figure 4, in order to reduce the water and dust effect is the test, a water and dust
filter device is used before the sensor that is installed in the field.
The NB-Internet of Things communication scheme is employed in order to achieve a realtime monitoring of the sensor data. This mine wireless laser methane sensor monitoring
system establishes the connection between the sensor and the remote monitor devices such
as a mobile phone, and the real-time monitoring of each sensor in the field can be achieved,
as the result, the real-time data of every sensor can be queried through the internet anywhere
in the world.
The data of the measured results are shown in Table 4 below.
The mine laser methane sensor accurately measures methane concentration, temperature
and pressure, and the measured results can be view globally with the use a mobile phone.
After a long-term operation, sensor system operation is stable and no abnormalities such as
data mutations and disconnections during the operation.
From the on-site operational results, it can be seen that the laser methane sensor developed
here is an ideal solution for gas drainage pipeline applications. The system has very good advantages when used in coal mine applications, especially where the installation location is remote.
Figure 4. Field installation diagram.
Table 4. The recorded operational data (pressure, temperature and methane concentration).
Recorded Operational Data
Pressure
:···,···JU!a ltll!IJJJI!I) tit l b!I I I U' :l •• tl . . 1!f'-ll<J
Temoerature
CH4 Concentration
i~
:..-::
;::;;;:;;::
ii
~ g ~~~
~!
#~ .. li
2~
=~
::::c:s:o;
u
::a: .. .. iii
n uu u .. u