

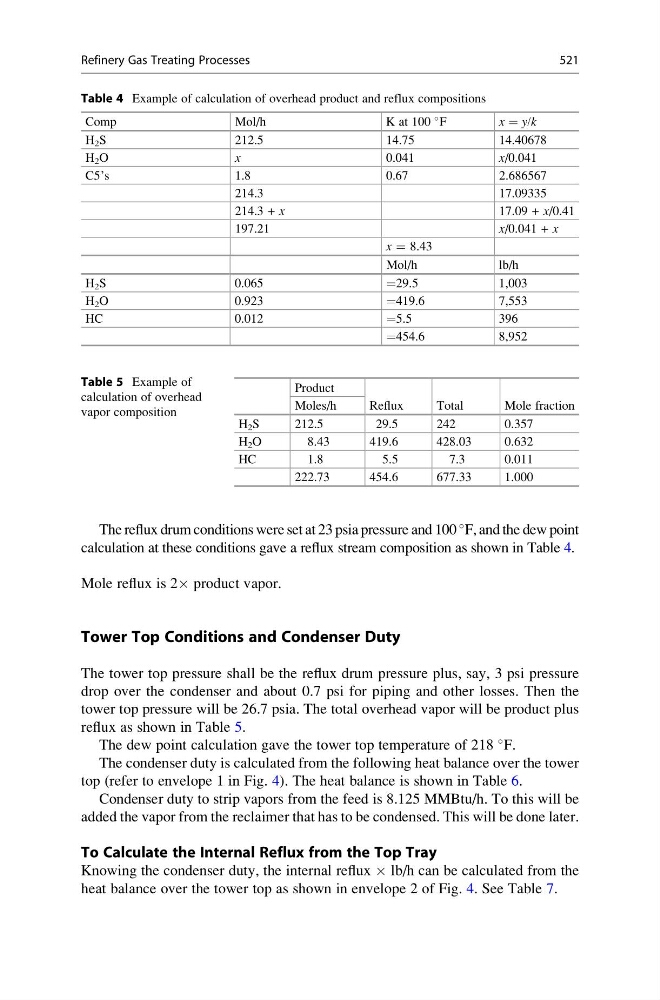
The reflux drum conditions were set at 23 psia pressure and 100
F, and the dew point
calculation at these conditions gave a reflux stream composition as shown in Table 4.
Mole reflux is 2Â product vapor.
Tower Top Conditions and Condenser Duty
The tower top pressure shall be the reflux drum pressure plus, say, 3 psi pressure
drop over the condenser and about 0.7 psi for piping and other losses. Then the
tower top pressure will be 26.7 psia. The total overhead vapor will be product plus
reflux as shown in Table 5.
The dew point calculation gave the tower top temperature of 218
F.
The condenser duty is calculated from the following heat balance over the tower
top (refer to envelope 1 in Fig. 4). The heat balance is shown in Table 6.
Condenser duty to strip vapors from the feed is 8.125 MMBtu/h. To this will be
added the vapor from the reclaimer that has to be condensed. This will be done later.
To Calculate the Internal Reflux from the Top Tray
Knowing the condenser duty, the internal reflux  lb/h can be calculated from the
heat balance over the tower top as shown in envelope 2 of Fig. 4. See Table 7.
Table 4 Example of calculation of overhead product and reflux compositions
Comp
Mol/h
K at 100
F
x = y/k
H 2 S
212.5
14.75
14.40678
H 2 O
x
0.041
x/0.041
C5’s
1.8
0.67
2.686567
214.3
17.09335
214.3 + x
17.09 + x/0.41
197.21
x/0.041 + x
x = 8.43
Mol/h
lb/h
H 2 S
0.065
=29.5
1,003
H 2 O
0.923
=419.6
7,553
HC
0.012
=5.5
396
=454.6
8,952
Table 5 Example of
calculation of overhead
vapor composition
Product
Reflux
Total
Mole fraction
Moles/h
H 2 S
212.5
29.5
242
0.357
H 2 O
8.43
419.6
428.03
0.632
HC
1.8
5.5
7.3
0.011
222.73
454.6
677.33
1.000
Refinery Gas Treating Processes
521