

overhead condenser duty. It must also be included in any tower loading exercise
that may follow. As noted previously, there are also proprietary methods for
reclaiming that do not involve a reclaimer/reboiler arrangement. These are provided
as a contract service and are beyond the scope of this handbook.
Appendix Process Design of an Amine Gas Treating Unit
The following is an extract from a design specification and defines the parameters
of this example:
1. Unit required is a gas treating unit for the removal of H 2 S from a hydrotreater
recycle gas stream. The feed to the hydrotreater consists of gas oil from straight
run source and streams from a thermal cracker and a catalytic cracker. The
recycle gas will therefore contain some COS.
2. The feed gas shall have the following properties:
• The mole weight of the gas is 10.5.
• The H 2 S content of feed gas is 4,048 grains/100 scf.
• The gas rate is 30 MMscf/day
• The pressure of the gas at the outlet of the contactor is 320 psig.
3. Product gas shall have a H 2 S content no greater than 0.1 grain/100 scf.
4. The amine solvent to be used shall be monoethanolamine:
• Amine ratio to H 2 S shall be 3.0 mole amine to 1.0 mole H 2 S.
• The amine solution shall be 20 % by weight in water.
• Residual H 2 S in the lean amine solution shall be no greater than 0.09 mole per
mole of MEA.
• Protection against degradation of the amine shall be included.
The Contactor Design
Calculating the Amine Solution Circulation Rate
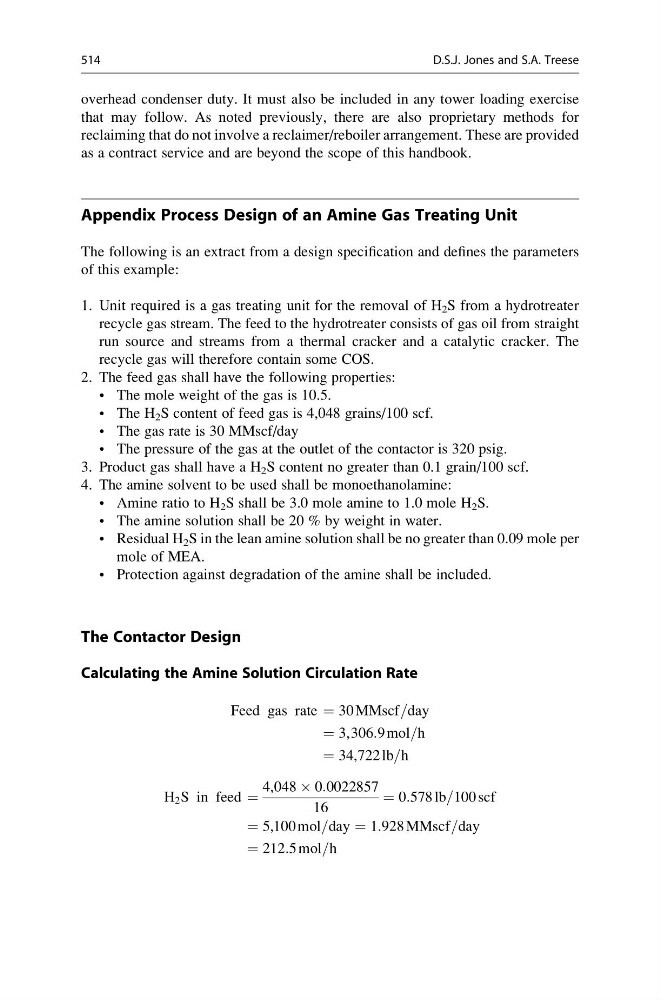
Feed gas rate ¼ 30 MMscf=day
¼ 3,306:9 mol=h
¼ 34,722 lb=h
H 2 S in feed ¼
4,048 Â 0:0022857
16
¼ 0:578 lb=100 scf
¼ 5,100 mol=day ¼ 1:928 MMscf=day
¼ 212:5 mol=h
514
D.S.J. Jones and S.A. Treese