

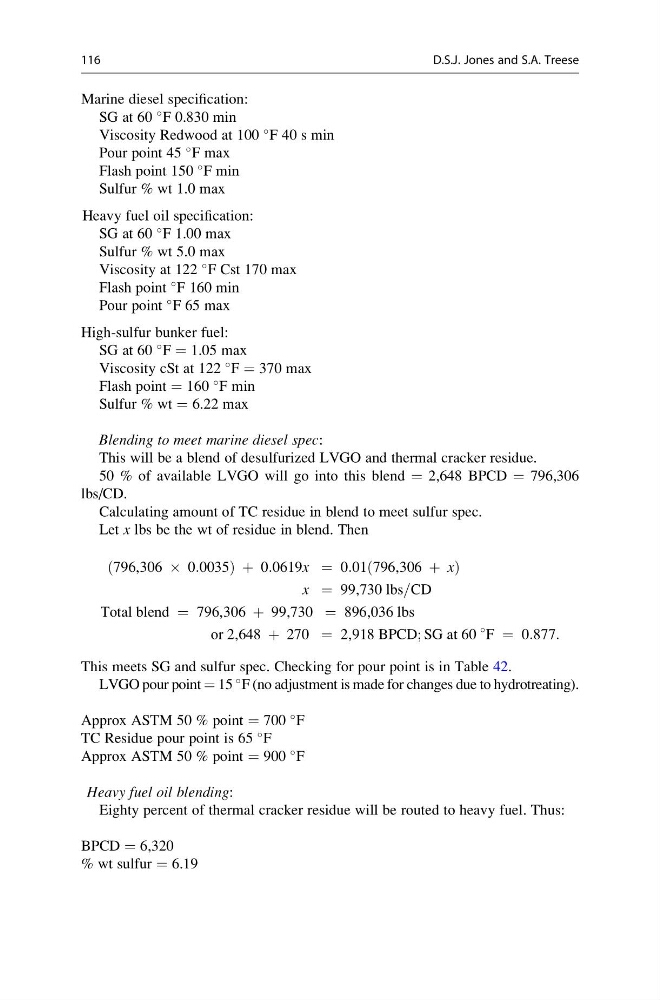
Marine diesel specification:
SG at 60
F 0.830 min
Viscosity Redwood at 100
F 40 s min
Pour point 45
F max
Flash point 150
F min
Sulfur % wt 1.0 max
Heavy fuel oil specification:
SG at 60
F 1.00 max
Sulfur % wt 5.0 max
Viscosity at 122
F Cst 170 max
Flash point
F 160 min
Pour point
F 65 max
High-sulfur bunker fuel:
SG at 60
F = 1.05 max
Viscosity cSt at 122
F = 370 max
Flash point = 160
F min
Sulfur % wt = 6.22 max
Blending to meet marine diesel spec:
This will be a blend of desulfurized LVGO and thermal cracker residue.
50 % of available LVGO will go into this blend = 2,648 BPCD = 796,306
lbs/CD.
Calculating amount of TC residue in blend to meet sulfur spec.
Let x lbs be the wt of residue in blend. Then
796,306 Â 0:0035
ð
Þ þ 0:0619x ¼ 0:01 796,306 þ x
ð
Þ
x ¼ 99,730 lbs=CD
Total blend ¼ 796,306 þ 99,730 ¼ 896,036 lbs
or 2,648 þ 270 ¼ 2,918 BPCD; SG at 60
F ¼ 0:877:
This meets SG and sulfur spec. Checking for pour point is in Table 42.
LVGO pour point = 15
F (no adjustment is made for changes due to hydrotreating).
Approx ASTM 50 % point = 700
F
TC Residue pour point is 65
F
Approx ASTM 50 % point = 900
F
Heavy fuel oil blending:
Eighty percent of thermal cracker residue will be routed to heavy fuel. Thus:
BPCD = 6,320
% wt sulfur = 6.19
116
D.S.J. Jones and S.A. Treese
SG at 60
F 0.830 min
Viscosity Redwood at 100
F 40 s min
Pour point 45
F max
Flash point 150
F min
Sulfur % wt 1.0 max
Heavy fuel oil specification:
SG at 60
F 1.00 max
Sulfur % wt 5.0 max
Viscosity at 122
F Cst 170 max
Flash point
F 160 min
Pour point
F 65 max
High-sulfur bunker fuel:
SG at 60
F = 1.05 max
Viscosity cSt at 122
F = 370 max
Flash point = 160
F min
Sulfur % wt = 6.22 max
Blending to meet marine diesel spec:
This will be a blend of desulfurized LVGO and thermal cracker residue.
50 % of available LVGO will go into this blend = 2,648 BPCD = 796,306
lbs/CD.
Calculating amount of TC residue in blend to meet sulfur spec.
Let x lbs be the wt of residue in blend. Then
796,306 Â 0:0035
ð
Þ þ 0:0619x ¼ 0:01 796,306 þ x
ð
Þ
x ¼ 99,730 lbs=CD
Total blend ¼ 796,306 þ 99,730 ¼ 896,036 lbs
or 2,648 þ 270 ¼ 2,918 BPCD; SG at 60
F ¼ 0:877:
This meets SG and sulfur spec. Checking for pour point is in Table 42.
LVGO pour point = 15
F (no adjustment is made for changes due to hydrotreating).
Approx ASTM 50 % point = 700
F
TC Residue pour point is 65
F
Approx ASTM 50 % point = 900
F
Heavy fuel oil blending:
Eighty percent of thermal cracker residue will be routed to heavy fuel. Thus:
BPCD = 6,320
% wt sulfur = 6.19
116
D.S.J. Jones and S.A. Treese