

5.6 Prototypical Implementation
135
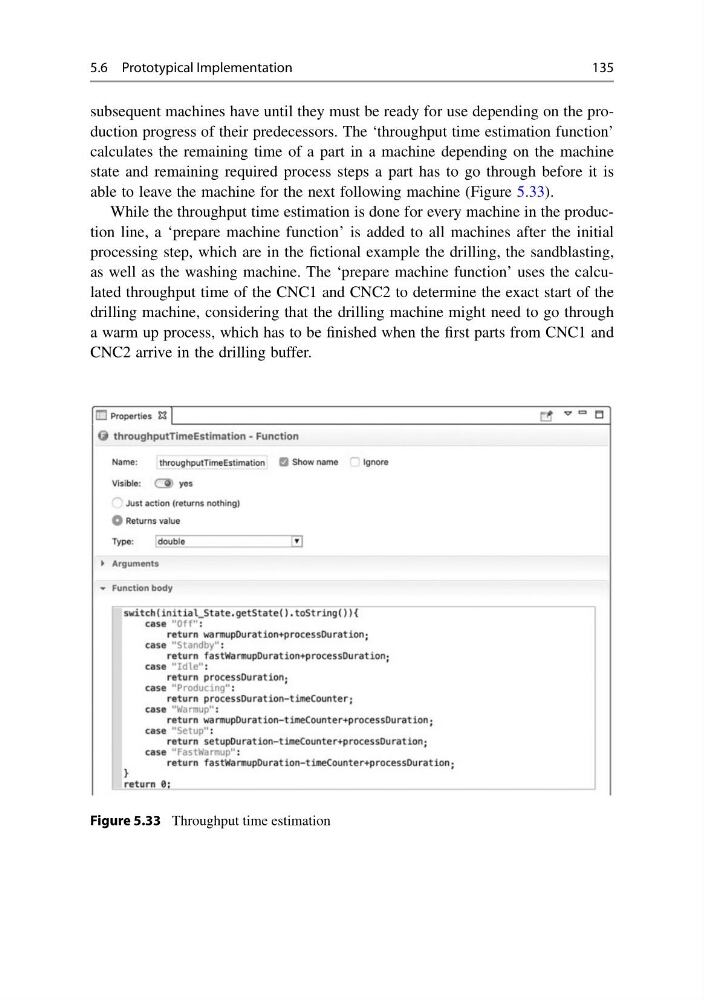
subsequent machines have until they must be ready for use depending on the production progress of their predecessors. The ‘throughput time estimation function’
calculates the remaining time of a part in a machine depending on the machine
state and remaining required process steps a part has to go through before it is
able to leave the machine for the next following machine (Figure 5.33).
While the throughput time estimation is done for every machine in the production line, a ‘prepare machine function’ is added to all machines after the initial
processing step, which are in the fictional example the drilling, the sandblasting,
as well as the washing machine. The ‘prepare machine function’ uses the calculated throughput time of the CNC1 and CNC2 to determine the exact start of the
drilling machine, considering that the drilling machine might need to go through
a warm up process, which has to be finished when the first parts from CNC1 and
CNC2 arrive in the drilling buffer.
Figure 5.33 Throughput time estimation