

Understanding the Mechanical Response of Friction Stir Welded …
57
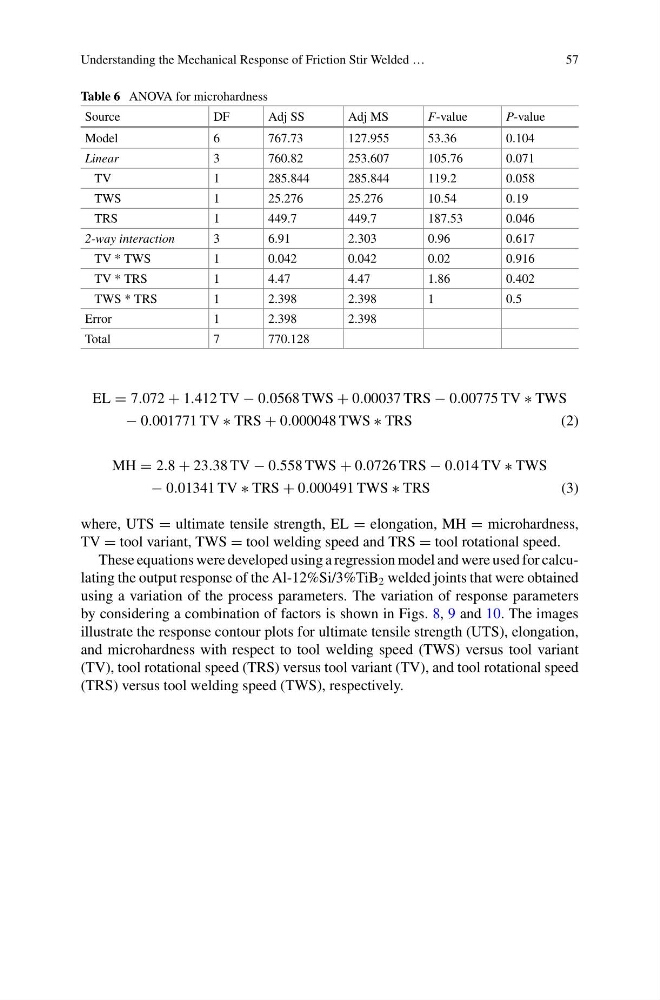
Table 6 ANOVA for microhardness
Source
DF
Adj SS
Adj MS
F-value
P-value
Model
6
767.73
127.955
53.36
0.104
Linear
3
760.82
253.607
105.76
0.071
TV
1
285.844
285.844
119.2
0.058
TWS
1
25.276
25.276
10.54
0.19
TRS
1
449.7
449.7
187.53
0.046
2-way interaction
3
6.91
2.303
0.96
0.617
TV * TWS
1
0.042
0.042
0.02
0.916
TV * TRS
1
4.47
4.47
1.86
0.402
TWS * TRS
1
2.398
2.398
1
0.5
Error
1
2.398
2.398
Total
7
770.128
EL = 7.072 + 1.412 TV − 0.0568 TWS + 0.00037 TRS − 0.00775 TV ∗ TWS
− 0.001771 TV ∗ TRS + 0.000048 TWS ∗ TRS
(2)
MH = 2.8 + 23.38 TV − 0.558 TWS + 0.0726 TRS − 0.014 TV ∗ TWS
− 0.01341 TV ∗ TRS + 0.000491 TWS ∗ TRS
(3)
where, UTS = ultimate tensile strength, EL = elongation, MH = microhardness,
TV = tool variant, TWS = tool welding speed and TRS = tool rotational speed.
These equations were developed using a regression model and were used for calculating the output response of the Al-12%Si/3%TiB 2 welded joints that were obtained
using a variation of the process parameters. The variation of response parameters
by considering a combination of factors is shown in Figs. 8, 9 and 10. The images
illustrate the response contour plots for ultimate tensile strength (UTS), elongation,
and microhardness with respect to tool welding speed (TWS) versus tool variant
(TV), tool rotational speed (TRS) versus tool variant (TV), and tool rotational speed
(TRS) versus tool welding speed (TWS), respectively.