

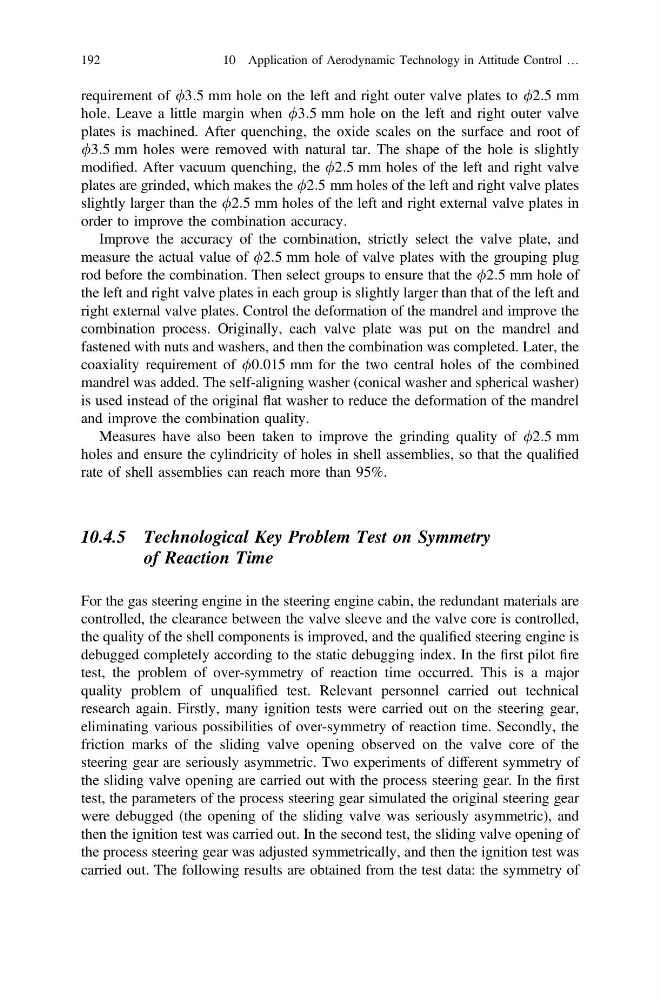
requirement of /3:5 mm hole on the left and right outer valve plates to /2:5 mm
hole. Leave a little margin when /3:5 mm hole on the left and right outer valve
plates is machined. After quenching, the oxide scales on the surface and root of
/3:5 mm holes were removed with natural tar. The shape of the hole is slightly
modified. After vacuum quenching, the /2:5 mm holes of the left and right valve
plates are grinded, which makes the /2:5 mm holes of the left and right valve plates
slightly larger than the /2:5 mm holes of the left and right external valve plates in
order to improve the combination accuracy.
Improve the accuracy of the combination, strictly select the valve plate, and
measure the actual value of /2:5 mm hole of valve plates with the grouping plug
rod before the combination. Then select groups to ensure that the /2:5 mm hole of
the left and right valve plates in each group is slightly larger than that of the left and
right external valve plates. Control the deformation of the mandrel and improve the
combination process. Originally, each valve plate was put on the mandrel and
fastened with nuts and washers, and then the combination was completed. Later, the
coaxiality requirement of /0:015 mm for the two central holes of the combined
mandrel was added. The self-aligning washer (conical washer and spherical washer)
is used instead of the original flat washer to reduce the deformation of the mandrel
and improve the combination quality.
Measures have also been taken to improve the grinding quality of /2:5 mm
holes and ensure the cylindricity of holes in shell assemblies, so that the qualified
rate of shell assemblies can reach more than 95%.
10.4.5 Technological Key Problem Test on Symmetry
of Reaction Time
For the gas steering engine in the steering engine cabin, the redundant materials are
controlled, the clearance between the valve sleeve and the valve core is controlled,
the quality of the shell components is improved, and the qualified steering engine is
debugged completely according to the static debugging index. In the first pilot fire
test, the problem of over-symmetry of reaction time occurred. This is a major
quality problem of unqualified test. Relevant personnel carried out technical
research again. Firstly, many ignition tests were carried out on the steering gear,
eliminating various possibilities of over-symmetry of reaction time. Secondly, the
friction marks of the sliding valve opening observed on the valve core of the
steering gear are seriously asymmetric. Two experiments of different symmetry of
the sliding valve opening are carried out with the process steering gear. In the first
test, the parameters of the process steering gear simulated the original steering gear
were debugged (the opening of the sliding valve was seriously asymmetric), and
then the ignition test was carried out. In the second test, the sliding valve opening of
the process steering gear was adjusted symmetrically, and then the ignition test was
carried out. The following results are obtained from the test data: the symmetry of
192
10 Application of Aerodynamic Technology in Attitude Control …