

6 Tool Model Building and Research on Cutting Simulation …
75
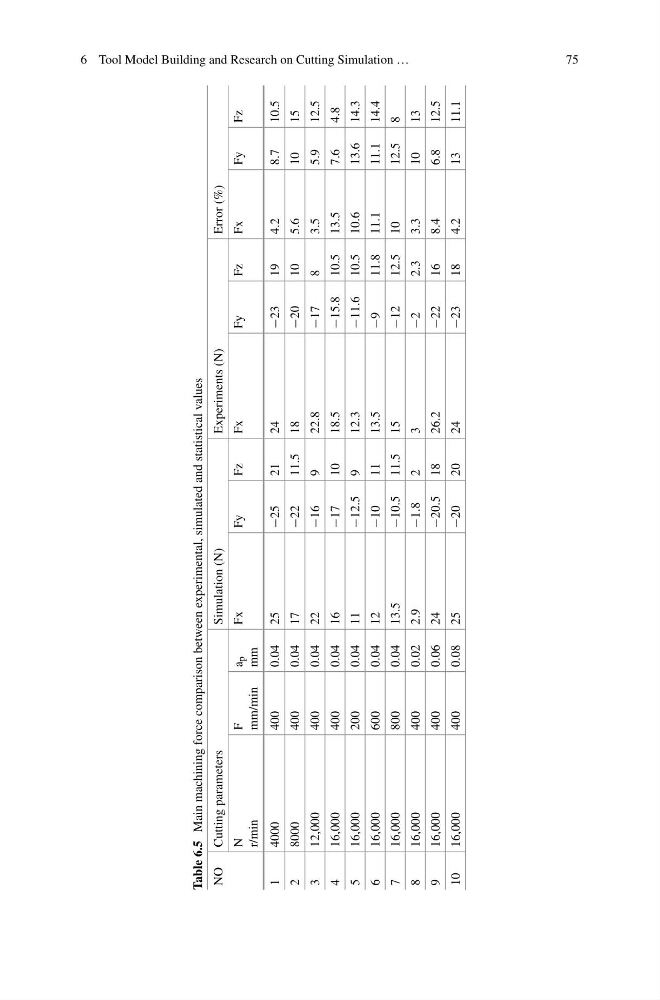
Table 6.5
Main machining force comparison between experimental, simulated and statistical values
NO
Cutting parameters
Simulation (N)
Experiments (N)
Error (%)
N
r/min
F
mm/min
a
p
mm
Fx
Fy
Fz
Fx
Fy
Fz
Fx
Fy
Fz
1
4000
400
0.04
25
−25
21
24
−23
19
4.2
8.7
10.5
2
8000
400
0.04
17
−22
11.5
18
−20
10
5.6
10
15
3
12,000
400
0.04
22
−16
9
22.8
−17
8
3.5
5.9
12.5
4
16,000
400
0.04
16
−17
10
18.5
−15.8
10.5
13.5
7.6
4.8
5
16,000
200
0.04
11
−12.5
9
12.3
−11.6
10.5
10.6
13.6
14.3
6
16,000
600
0.04
12
−10
11
13.5
−9
11.8
11.1
11.1
14.4
7
16,000
800
0.04
13.5
−10.5
11.5
15
−12
12.5
10
12.5
8
8
16,000
400
0.02
2.9
−1.8
2
3
−2
2.3
3.3
10
13
9
16,000
400
0.06
24
−20.5
18
26.2
−22
16
8.4
6.8
12.5
10
16,000
400
0.08
25
−20
20
24
−23
18
4.2
13
11.1