

the softening point of the glass without causing a collapse of the bulb helping
to evenly distribute strains and distortion forces. Once the desired level of
exhaustion was reached the tubulatures were sealed by fusion
57 using electrical heating elements at the base of the lamps. Sealed and cooled, the lead
58
wires from the filament were soldered to the lamp base, and the base baked
onto the bulb. Quite ingenious.
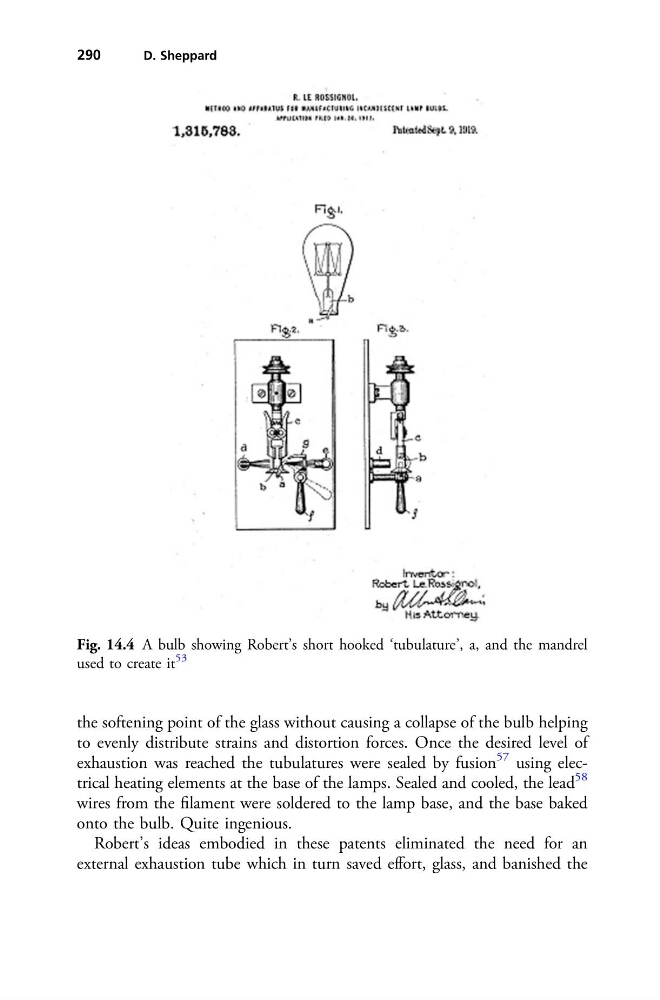
Robert’s ideas embodied in these patents eliminated the need for an
external exhaustion tube which in turn saved effort, glass, and banished the
Fig. 14.4 A bulb showing Robert’s short hooked ‘tubulature’, a, and the mandrel
used to create it
53
290
D. Sheppard