

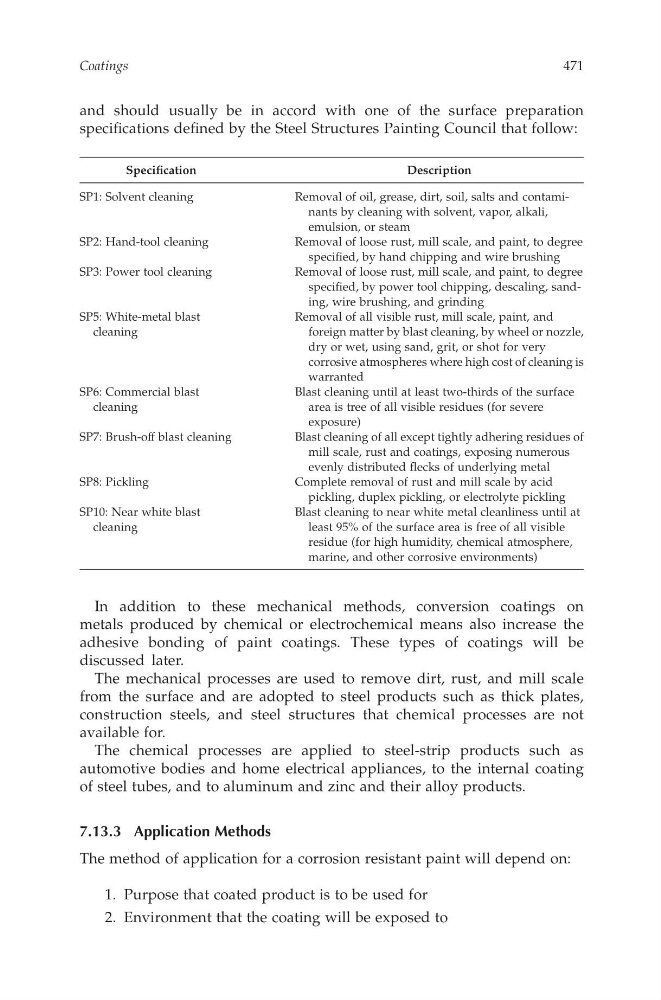
and should usuallyb ei na ccord with one of the surface preparation
specificationsd efined by the SteelS tructures Painting Council that follow:
Specification
Description
SP1: Solvent cleaning
Removal of oil, grease, dirt, soil, salts and contaminants by cleaning with solvent, vapor,alkali,
emulsion, or steam
SP2: Hand-tool cleaning
Removal of loose rust, mill scale, and paint, to degree
specified, by hand chipping and wire brushing
SP3: Power tool cleaning
Removal of loose rust, mill scale, and paint, to degree
specified, by power tool chipping, descaling, sanding, wireb rushing, and grinding
SP5: White-metal blast
cleaning
Removal of all visible rust, mill scale, paint, and
foreign matter by blast cleaning, by wheel or nozzle,
dry or wet, using sand, grit, or shot for very
corrosive atmospheres wherehigh cost of cleaning is
warranted
SP6: Commercial blast
cleaning
Blast cleaning until at least two-thirds of the surface
area is tree of all visible residues (for severe
exposure)
SP7: Brush-offblast cleaning
Blast cleaning of all except tightly adhering residues of
mill scale, rust and coatings, exposing numerous
evenly distributed flecks of underlying metal
SP8: Pickling
Complete removal of rust and mill scale by acid
pickling, duplex pickling, or electrolyte pickling
SP10: Near white blast
cleaning
Blast cleaning to near white metal cleanliness until at
least 95% of the surface areaisfree of all visible
residue (for high humidity,chemicalatmosphere,
marine, and other corrosive environments)
In addition to these mechanical methods,c onversion coatings on
metals produced by chemical or electrochemical means also increase the
adhesive bonding of paintc oatings. These types of coatings will be
discussedl ater.
The mechanical processes are used to remove dirt, rust, and mill scale
from the surface and are adopted to steel products such as thick plates,
construction steels, and steel structures that chemical processes are not
available for.
The chemical processes are applied to steel-strip products sucha s
automotive bodies and home electrical appliances, to the internal coating
of steel tubes, and to aluminum and zinc and their alloy products.
7.13.3A pplication Methods
The method of applicationfor acorrosionresistant paintwilld epend on:
1. Purpose that coated product is to be used for
2. Environment that the coating will be exposed to
Coatings
471
CAT8247—CHAPTER 7—17/10/2006—15:04—TRGANESH—XMLM ODEL B–pp. 403–485