

32 Prediction of Width and Thickness of Injection Molded …
461
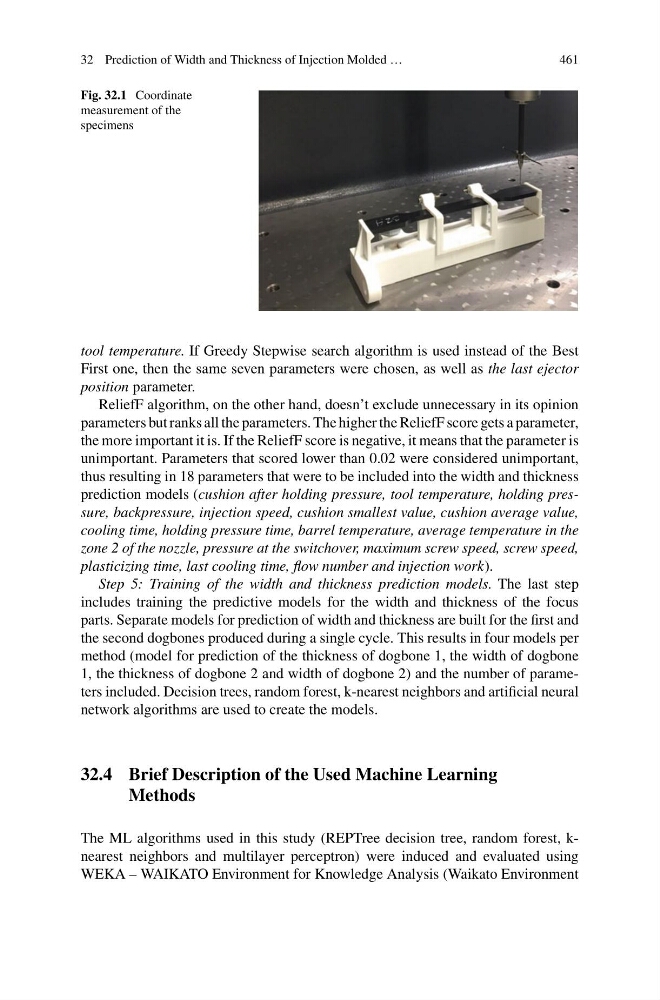
Fig. 32.1 Coordinate
measurement of the
specimens
tool temperature. If Greedy Stepwise search algorithm is used instead of the Best
First one, then the same seven parameters were chosen, as well as the last ejector
position parameter.
ReliefF algorithm, on the other hand, doesn’t exclude unnecessary in its opinion
parameters but ranks all the parameters. The higher the ReliefF score gets a parameter,
the more important it is. If the ReliefF score is negative, it means that the parameter is
unimportant. Parameters that scored lower than 0.02 were considered unimportant,
thus resulting in 18 parameters that were to be included into the width and thickness
prediction models (cushion after holding pressure, tool temperature, holding pressure, backpressure, injection speed, cushion smallest value, cushion average value,
cooling time, holding pressure time, barrel temperature, average temperature in the
zone 2 of the nozzle, pressure at the switchover, maximum screw speed, screw speed,
plasticizing time, last cooling time, flow number and injection work).
Step 5: Training of the width and thickness prediction models. The last step
includes training the predictive models for the width and thickness of the focus
parts. Separate models for prediction of width and thickness are built for the first and
the second dogbones produced during a single cycle. This results in four models per
method (model for prediction of the thickness of dogbone 1, the width of dogbone
1, the thickness of dogbone 2 and width of dogbone 2) and the number of parameters included. Decision trees, random forest, k-nearest neighbors and artificial neural
network algorithms are used to create the models.
32.4 Brief Description of the Used Machine Learning
Methods
The ML algorithms used in this study (REPTree decision tree, random forest, knearest neighbors and multilayer perceptron) were induced and evaluated using
WEKA – WAIKATO Environment for Knowledge Analysis (Waikato Environment