

206
M. S. Dani and I. B. Dave
0
2
4
6
8
10
12
14
Die Cast AZ91
Mg alloy
AZ91 FSP 380
SP with Al
AZ91 FSP 545
SP with Al
AZ91 FSP 380
DP with Al
AZ91 FSP 545
DP with Al
Grain size No
Grain Size Measurment
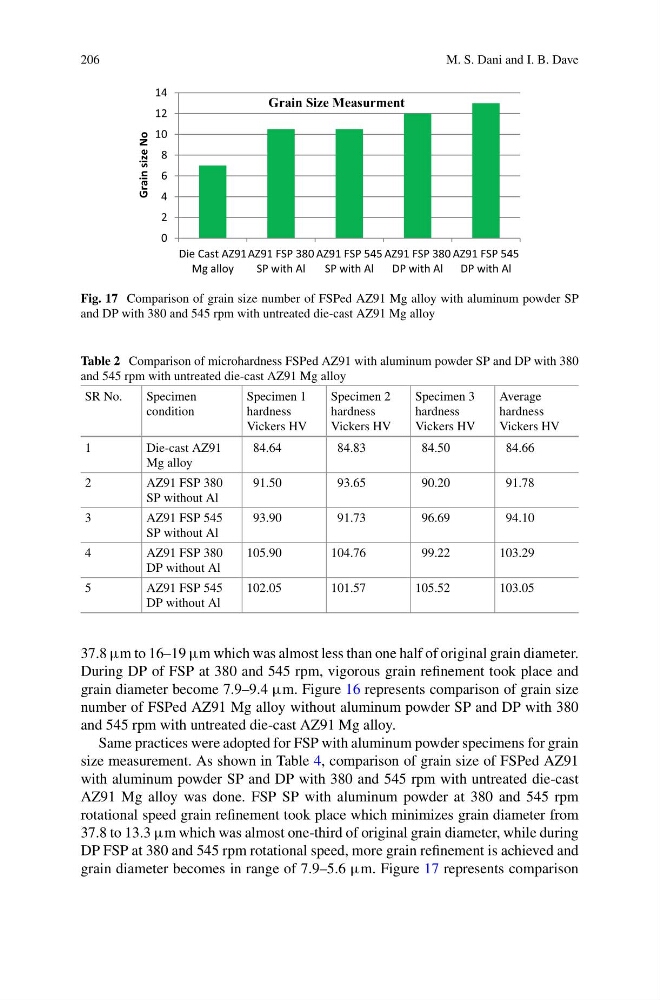
Fig. 17 Comparison of grain size number of FSPed AZ91 Mg alloy with aluminum powder SP
and DP with 380 and 545 rpm with untreated die-cast AZ91 Mg alloy
Table 2 Comparison of microhardness FSPed AZ91 with aluminum powder SP and DP with 380
and 545 rpm with untreated die-cast AZ91 Mg alloy
SR No.
Specimen
condition
Specimen 1
hardness
Vickers HV
Specimen 2
hardness
Vickers HV
Specimen 3
hardness
Vickers HV
Average
hardness
Vickers HV
1
Die-cast AZ91
Mg alloy
84.64
84.83
84.50
84.66
2
AZ91 FSP 380
SP without Al
91.50
93.65
90.20
91.78
3
AZ91 FSP 545
SP without Al
93.90
91.73
96.69
94.10
4
AZ91 FSP 380
DP without Al
105.90
104.76
99.22
103.29
5
AZ91 FSP 545
DP without Al
102.05
101.57
105.52
103.05
37.8 μm to 16–19 μm which was almost less than one half of original grain diameter.
During DP of FSP at 380 and 545 rpm, vigorous grain refinement took place and
grain diameter become 7.9–9.4 μm. Figure 16 represents comparison of grain size
number of FSPed AZ91 Mg alloy without aluminum powder SP and DP with 380
and 545 rpm with untreated die-cast AZ91 Mg alloy.
Same practices were adopted for FSP with aluminum powder specimens for grain
size measurement. As shown in Table 4, comparison of grain size of FSPed AZ91
with aluminum powder SP and DP with 380 and 545 rpm with untreated die-cast
AZ91 Mg alloy was done. FSP SP with aluminum powder at 380 and 545 rpm
rotational speed grain refinement took place which minimizes grain diameter from
37.8 to 13.3 μm which was almost one-third of original grain diameter, while during
DP FSP at 380 and 545 rpm rotational speed, more grain refinement is achieved and
grain diameter becomes in range of 7.9–5.6 μm. Figure 17 represents comparison