

98
A. Petare et al.
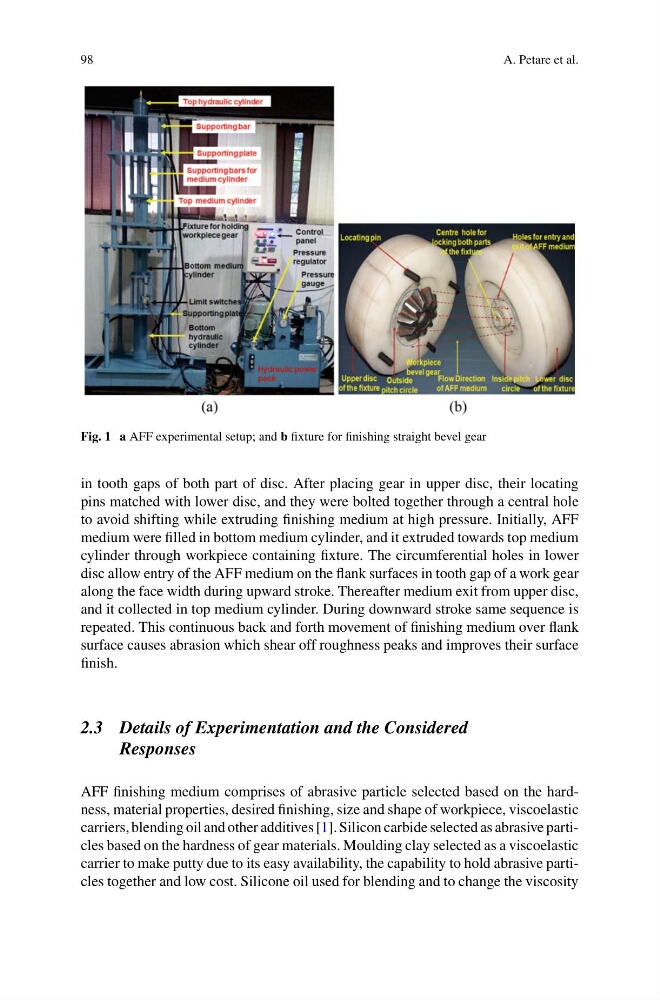
Fig. 1 a AFF experimental setup; and b fixture for finishing straight bevel gear
in tooth gaps of both part of disc. After placing gear in upper disc, their locating
pins matched with lower disc, and they were bolted together through a central hole
to avoid shifting while extruding finishing medium at high pressure. Initially, AFF
medium were filled in bottom medium cylinder, and it extruded towards top medium
cylinder through workpiece containing fixture. The circumferential holes in lower
disc allow entry of the AFF medium on the flank surfaces in tooth gap of a work gear
along the face width during upward stroke. Thereafter medium exit from upper disc,
and it collected in top medium cylinder. During downward stroke same sequence is
repeated. This continuous back and forth movement of finishing medium over flank
surface causes abrasion which shear off roughness peaks and improves their surface
finish.
2.3 Details of Experimentation and the Considered
Responses
AFF finishing medium comprises of abrasive particle selected based on the hardness, material properties, desired finishing, size and shape of workpiece, viscoelastic
carriers, blending oil and other additives [1]. Silicon carbide selected as abrasive particles based on the hardness of gear materials. Moulding clay selected as a viscoelastic
carrier to make putty due to its easy availability, the capability to hold abrasive particles together and low cost. Silicone oil used for blending and to change the viscosity